Alfa Laval Heat Exchangers For Wisconsin RNG Plant
Spiral Heat Exchangers Deliver Energy Savings, Increased Uptime, Ease Of Maintenance At Wisconsin Dairy Farm
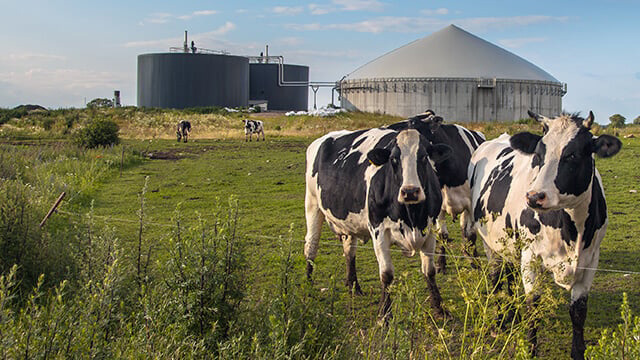
(Image Courtesy Of Alfa Laval)
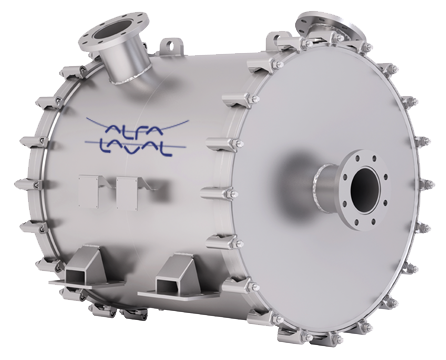
Manure mixed with bedding is a feedstock with varying viscosity and can contain up to 10% solids. This poses significant challenges at Freedom RNG. The piping both upstream and downstream of the heat exchangers has been subjected to clogging on different occasions due to the fibrous nature of the feedstock. Despite these challenges, Alfa Laval said that its spiral heat exchangers keep on performing.
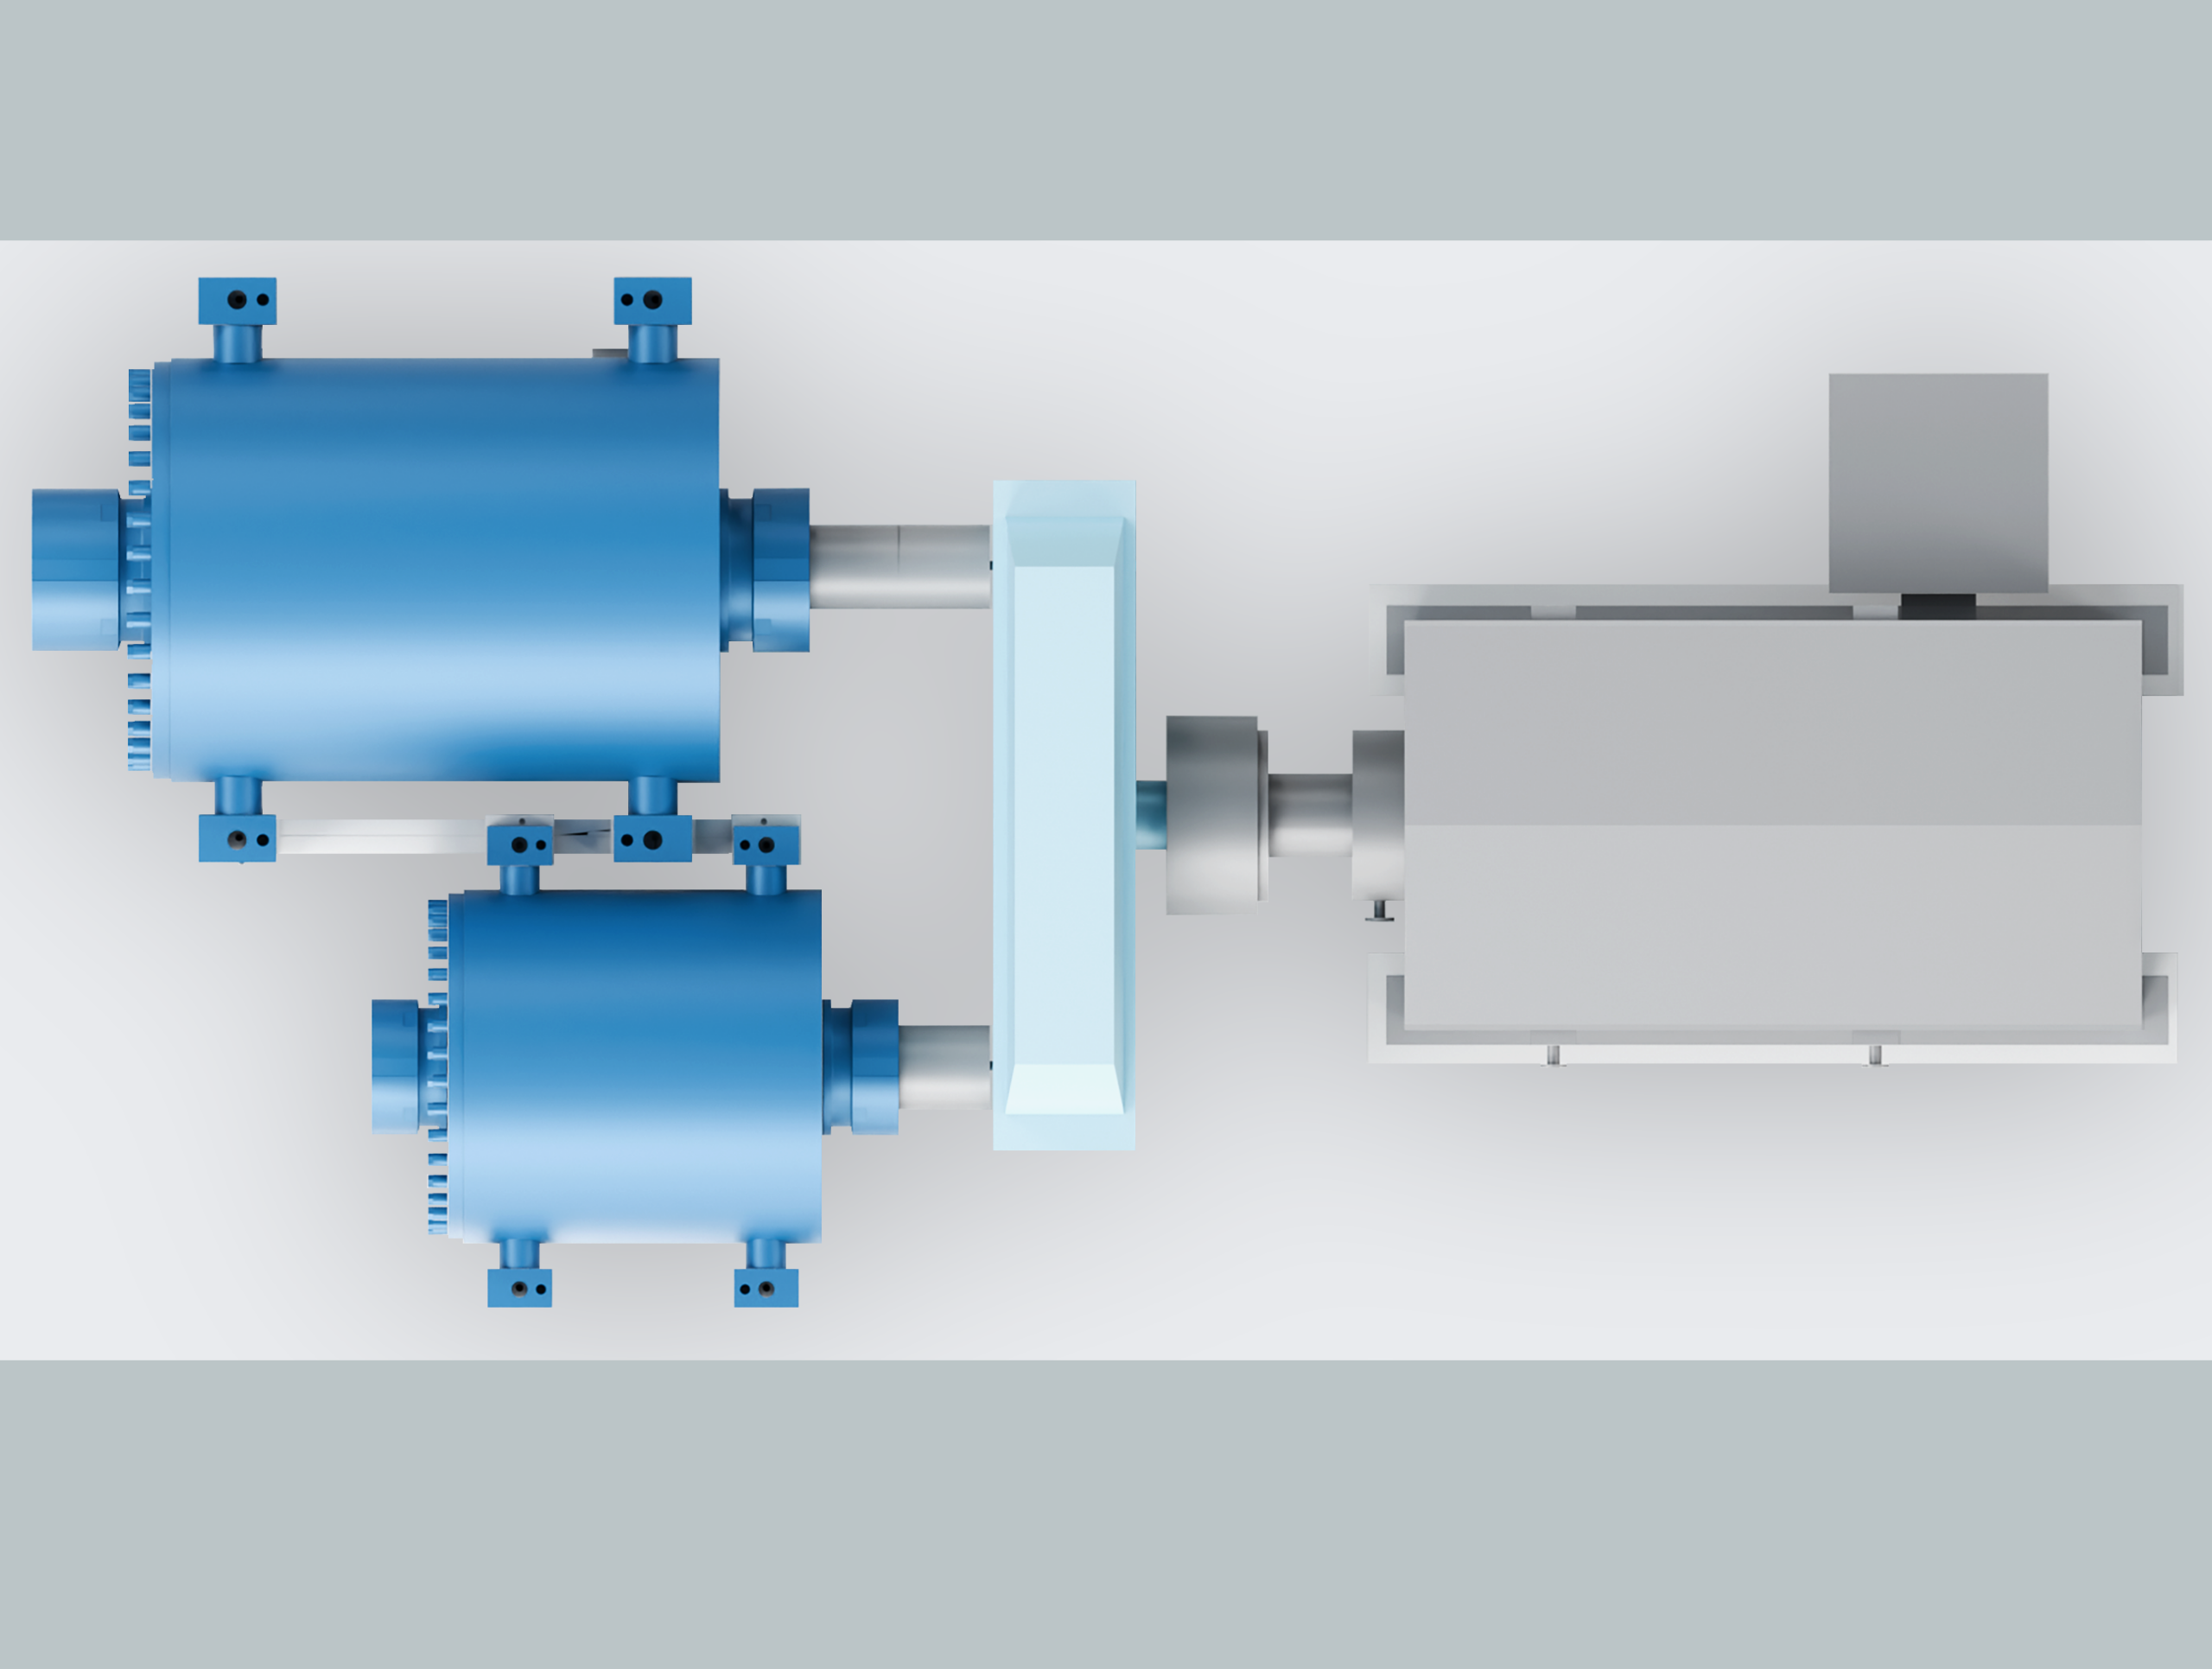
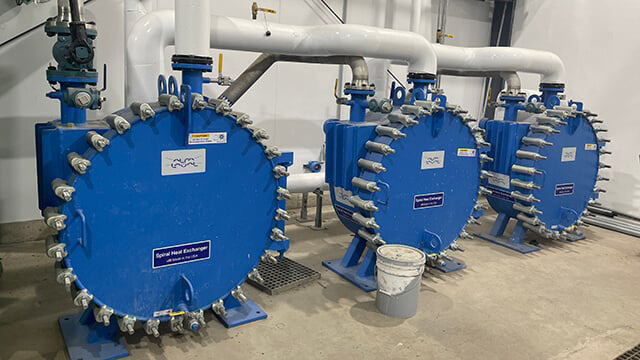
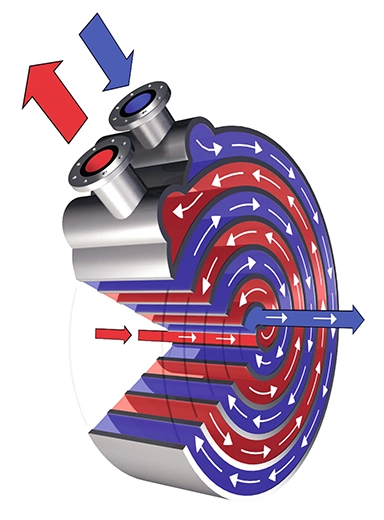
The continual curving, single-channel geometry creates high turbulence, minimizing fouling and clogging from the start. If fouling does occur, the self-clean design increases local velocity, creating a scrubbing effect that flushes away deposits.
(Image Courtesy Of Alfa Laval)
(Image Courtesy Of Alfa Laval)
“Since we started our trials, there has actually been no need for regular cleaning, which is a significant advantage over expectations,” says Kristopher Kreh, director of engineering at US Energy. “We anticipated having to clean the exchangers every four to six weeks. However, after 18 months of continuous operation, the units have remained clog-free and have required no maintenance, aside from routine inspections confirming their clean condition.”
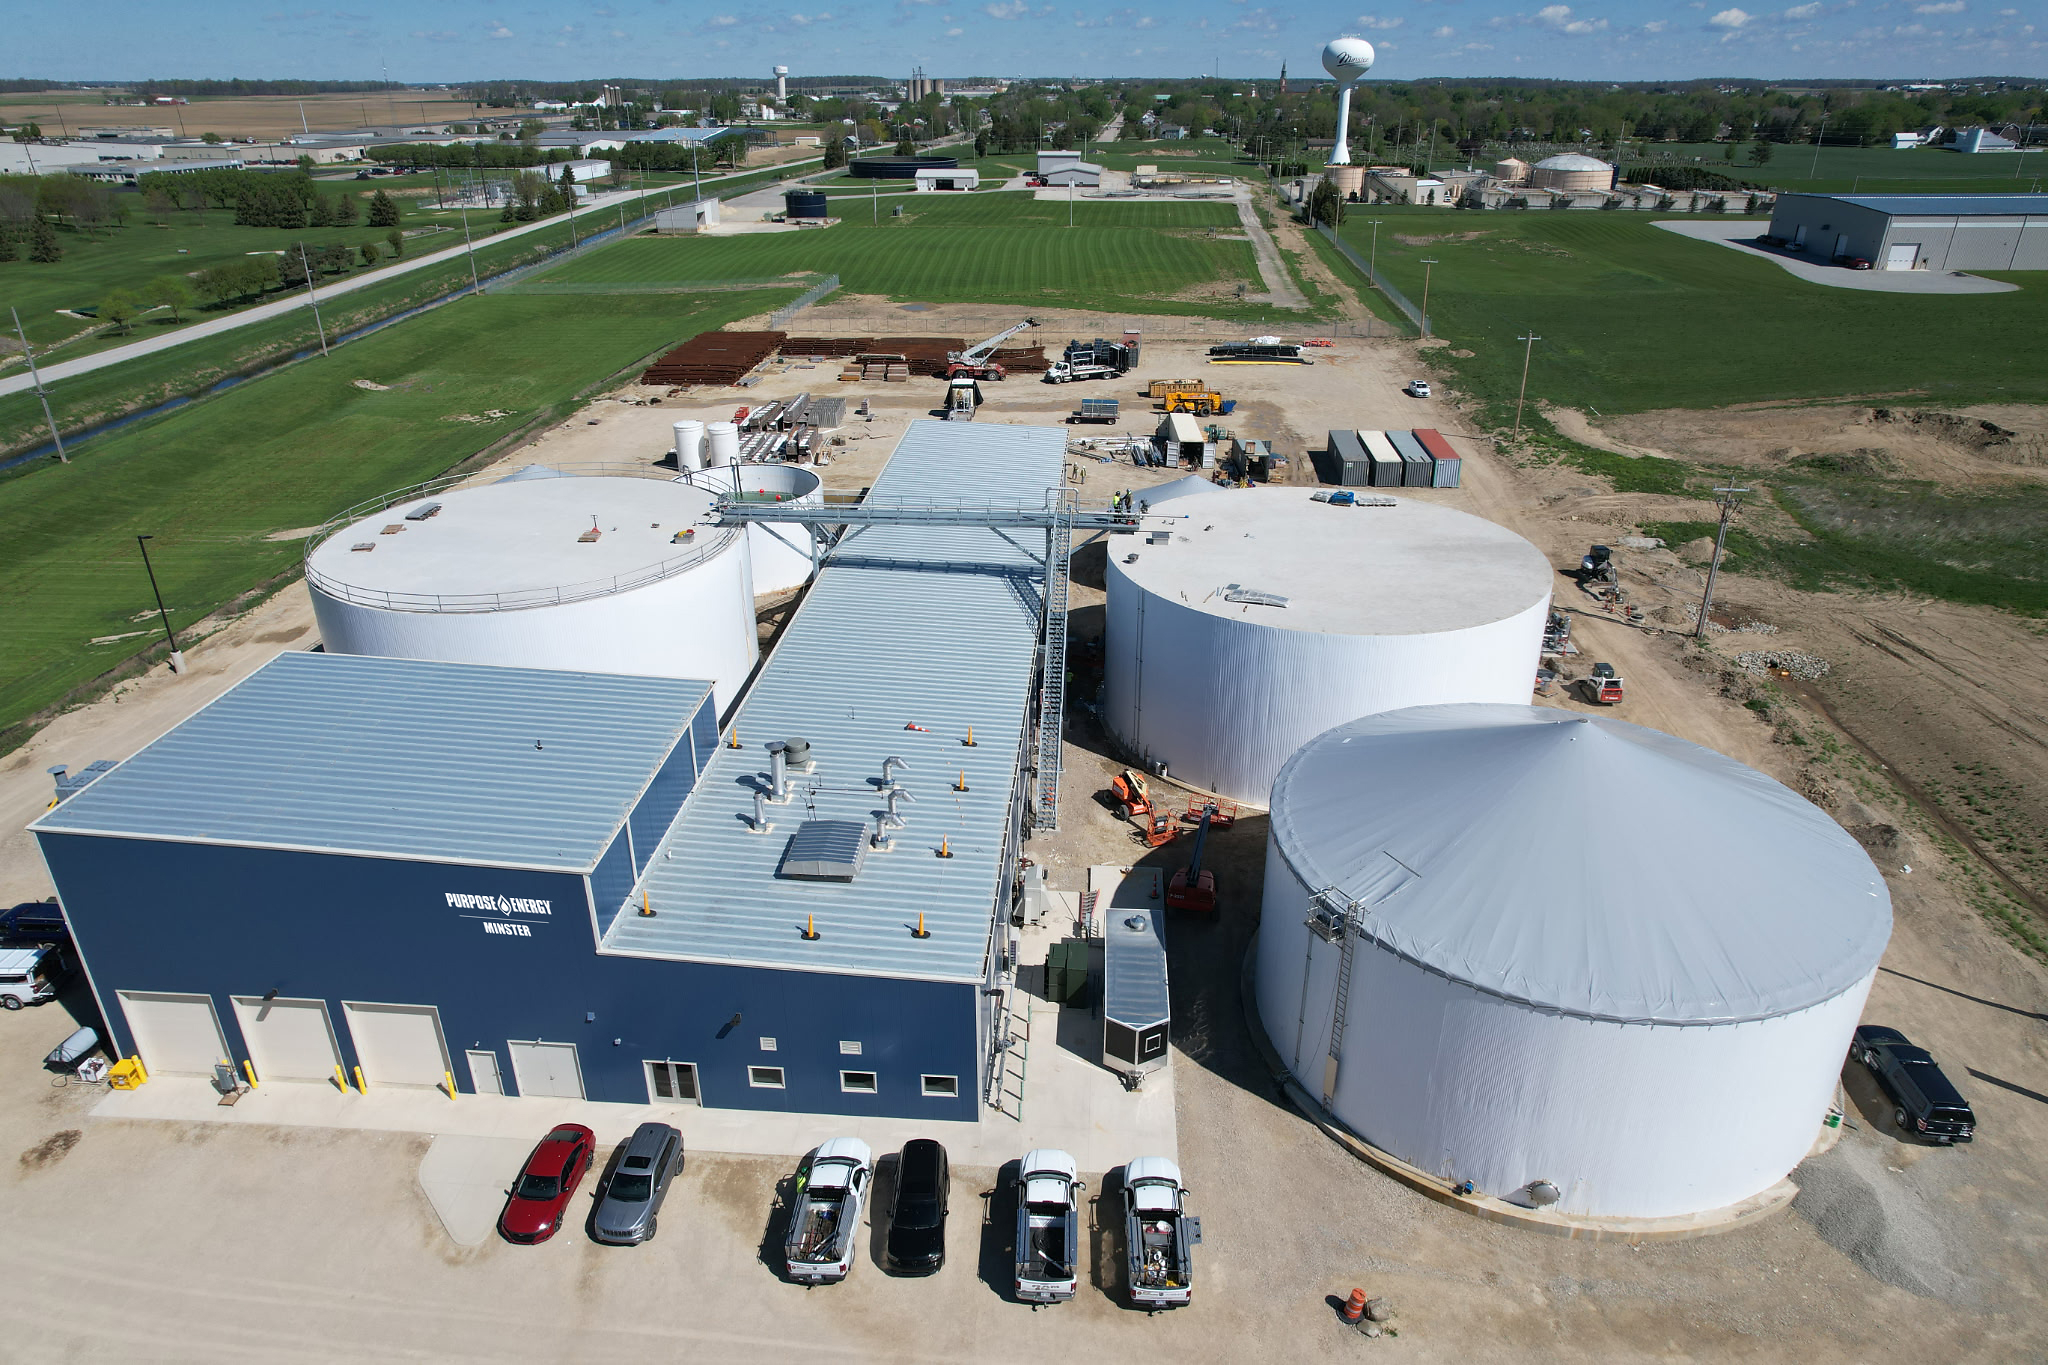
The dairy’s scraped output from the barn includes animal bedding and manure. These materials serve as feedstock for Freedom RNG, a new installation designed to produce 720,000 scf/d (20,400 m3 per day) of biomethane. The facility operates six Alfa Laval spiral heat exchangers that are delivering a technological solution in challenging conditions and offering peace of mind to US Energy in its operations.
“The reason for selecting spiral technology was its higher heat transfer efficiency, with the ease of maintenance being the icing on the cake,” said Kreh.
Freedom RNG has taken significant steps to improve the efficiency of its RNG production by operating with a two-stage digester and increase the gas output. The two-stage digester consists of one stage at hyperthermophilic temperatures and the second at mesophilic, which means they first need to heat up the manure and then cool it down again. This is where Alfa Laval said that its versatile spiral technology thrived.
(Image Courtesy Of Alfa Laval)
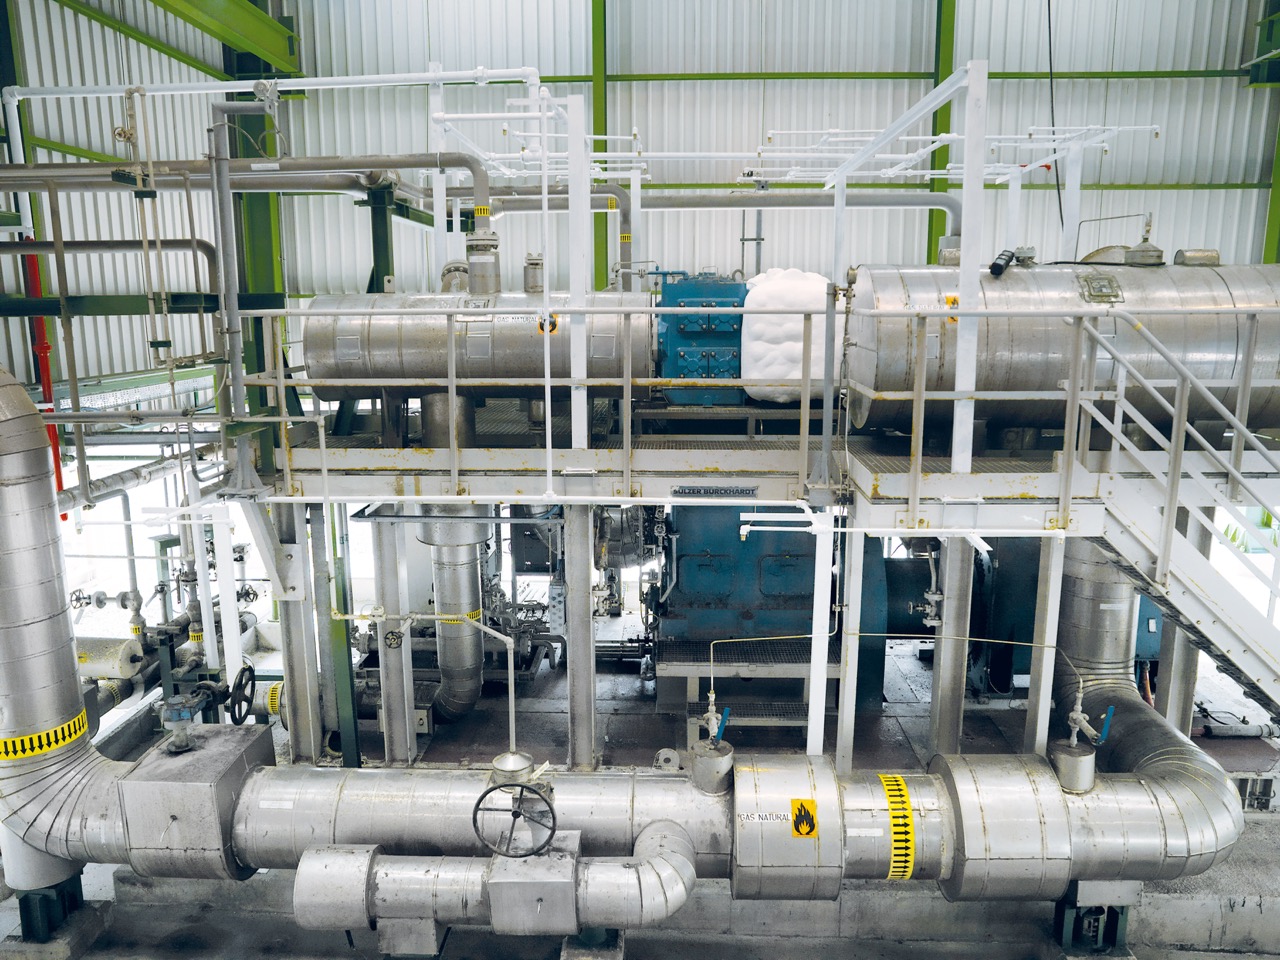
Three of the heat exchangers run sludge-to-water to heat the manure to reach the hyperthermophilic temperature of 165°F (74°C). The other three operate sludge-to-sludge, recovering heat to the incoming sludge, while cooling down the digested sludge before it goes into the lower temperature mesophilic stage. At Freedom RNG, these sludge-to-sludge spirals serve up savings of 2 MMBtu per hour and 96 tons (87 tonnes) of carbon dioxide equivalent per year.
“Our spiral heat exchangers have outperformed initial expectations, proving to be a game-changer in the RNG industry,” said Kreh. “They allow the process to run smoothly and efficiently, which is exactly what facilities need as they expand. We’re really excited to see how this technology can help more sites surpass their goals.”